Gear wheels, planetary gears, chain wheels, pump rings, individual cams, and wave generators: These workpieces are produced in millions for medium and large series manufacturing. After hardening, each workpiece undergoes a finishing process where dimensional accuracy, surface quality, and positional tolerances must be maintained simultaneously. With the VL 100 GT, EMAG offers a vertical turning and grinding center that combines hard turning, internal grinding, and external grinding for workpieces with a diameter of up to 100 mm in a single setup - with a footprint of around 9.6 square meters.
Vertical design and MINERALIT machine bed
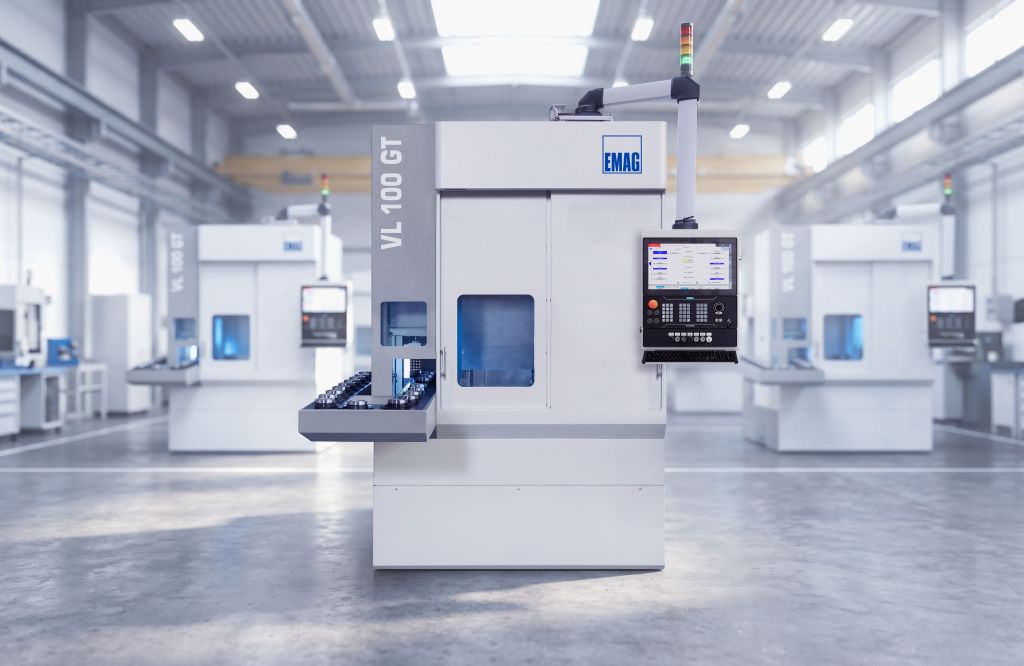
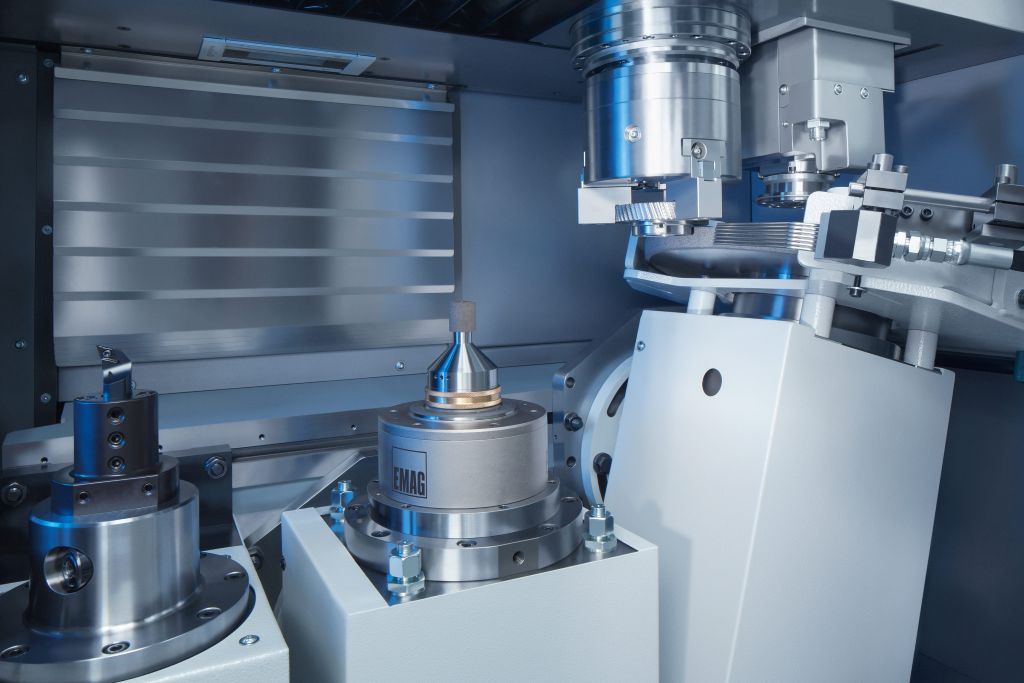
The VL 100 GT operates according to the vertical machining principle: The workpiece spindle is positioned above the working area and picks up the workpieces using a pick-up method from the integrated conveyor belt. Chips and grinding sludge fall freely downwards due to gravity, without accumulating on the workpiece or the guideways. This reduces thermal disturbances, avoids surface damage, and lowers cleaning efforts.
User-friendliness is also a priority with the VL 100 GT: The ergonomically designed working area allows for short setup times, and the compact footprint enables multi-machine operation.
The machine bed is made of the polymer concrete MINERALIT, which has eight times higher vibration damping compared to conventional gray cast iron. In finishing, where surface values in the range of Rz < 1.2 µm are required, this damping is a quality-determining factor. The achievable surfaces are free of swirl and meet the requirements for highly stressed functional surfaces in gears.
Integrated Pick-up Automation The main spindle takes care of loading and unloading itself: It travels to the pick-up station, picks up a raw part from the circulating conveyor belt of the O-Automation, moves it into the working area, returns the finished part after processing, and immediately picks up the next raw part. Separate loading robots or gantry loaders are eliminated, as are the associated investment costs. The short travel distances ensure very short chip-to-chip times.
Alternatively, the VL 100 GT can be equipped with shuttle automation for linked production lines. In combination with EMAG lathes from the VL or VT series, it is suitable for manufacturing systems from soft turning to hard fine machining.
Freely configurable working area
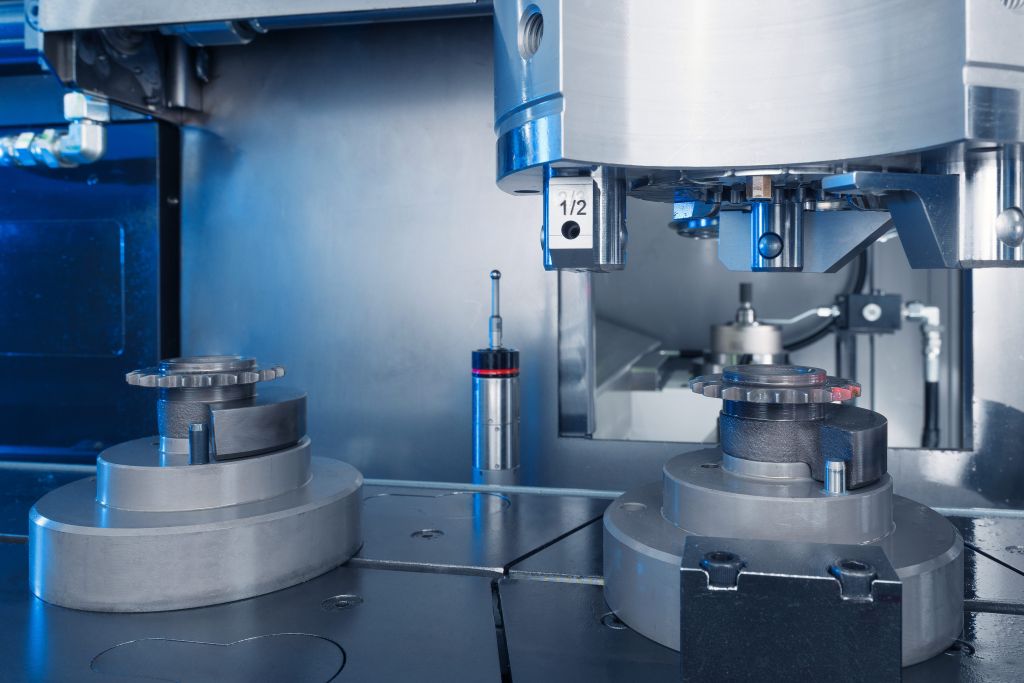
The working area is tailored to the specific workpiece spectrum in coordination with the customer. Available are internal grinding spindles for bores (corundum or CBN), external grinding spindles for cylindrical surfaces, flat shoulders, and contours, as well as one or two block steel holders for hard turning operations. This results in configurations from pure internal grinding to a combination of turning and grinding to complete machining with turning, internal grinding, and external grinding in a single setup.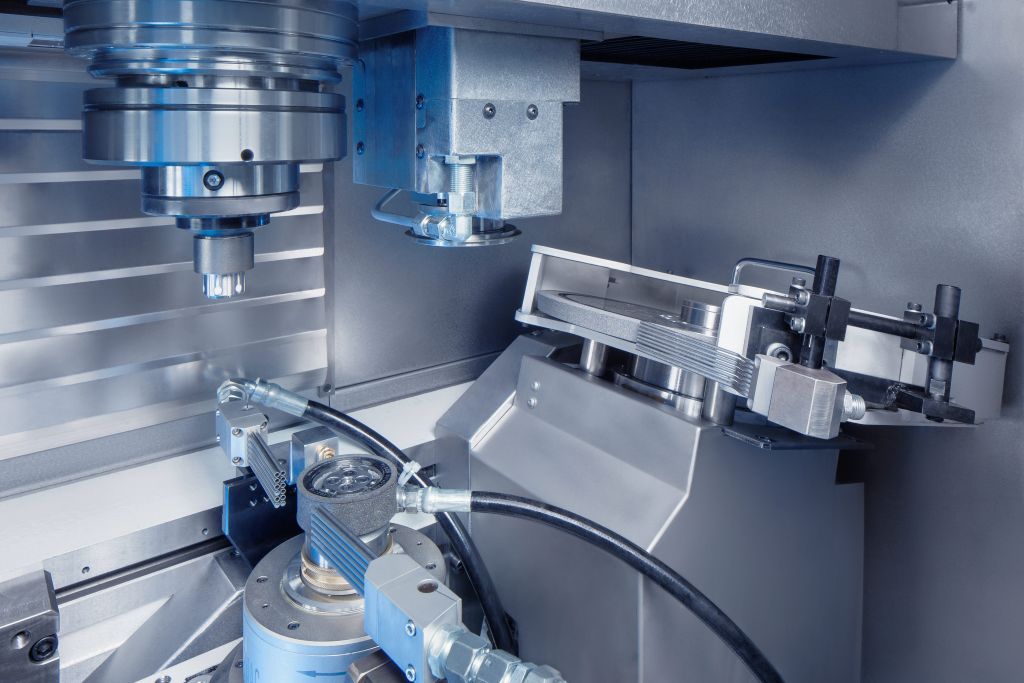
A linear motor drive in the X-axis enables the eccentric grinding of cam profiles and eccentric surfaces. Since the direct drive has no backlash due to its construction, form errors during the constant direction changes of the axis are avoided. This is a significant advantage over ball screw drives. Additionally, higher acceleration values and a wear-free operation are achieved.
Combination machining: Cost-effectiveness and quality
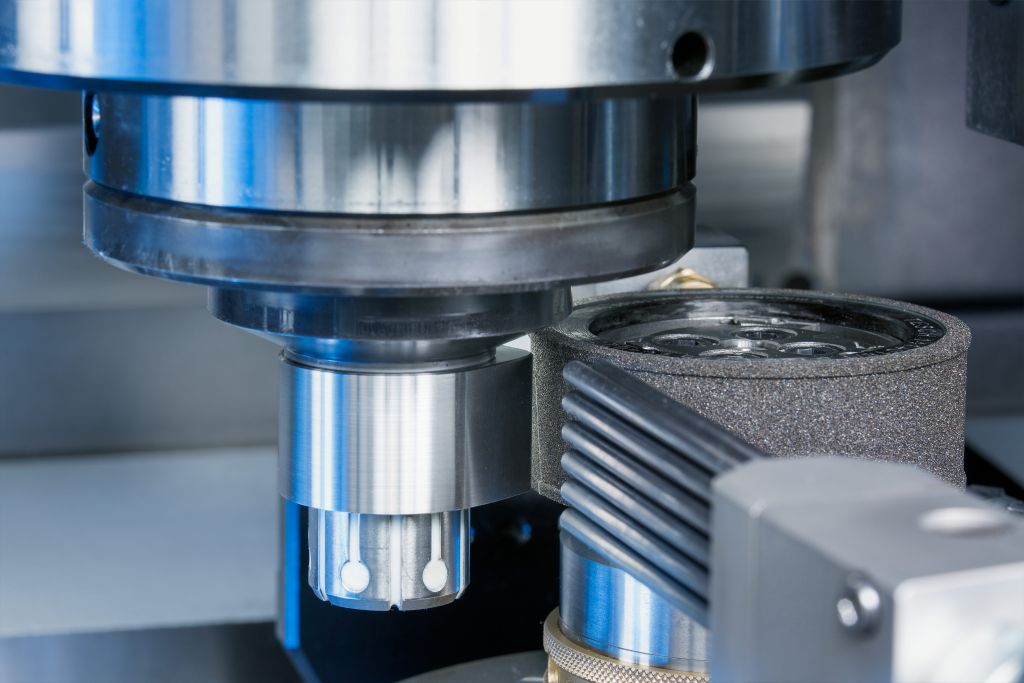
The combination of hard turning and grinding in a single setup is a central advantage of the VL 100 GT. In the first step, flat surfaces, chamfers, and grooves are produced by hard turning. The turning process is significantly faster than comparable operations in grinding. Subsequently, the high-precision geometry elements, such as bores, outer diameters, and running surfaces, are finished ground in the same setup.
The hard pre-turning leaves only a few micrometers of residual material for the grinding process. This approach significantly reduces the total processing time and completely eliminates setup errors, ensuring the positional relationships between the machined surfaces with the highest accuracy. The low material removal during grinding reduces wheel wear, extends dressing intervals, and lowers tool costs. At the same time, the amount of grinding sludge decreases, minimizing disposal costs and simplifying coolant preparation. In certain configurations, dry machining is possible.
Grinding sensors, process control, and measurement technology
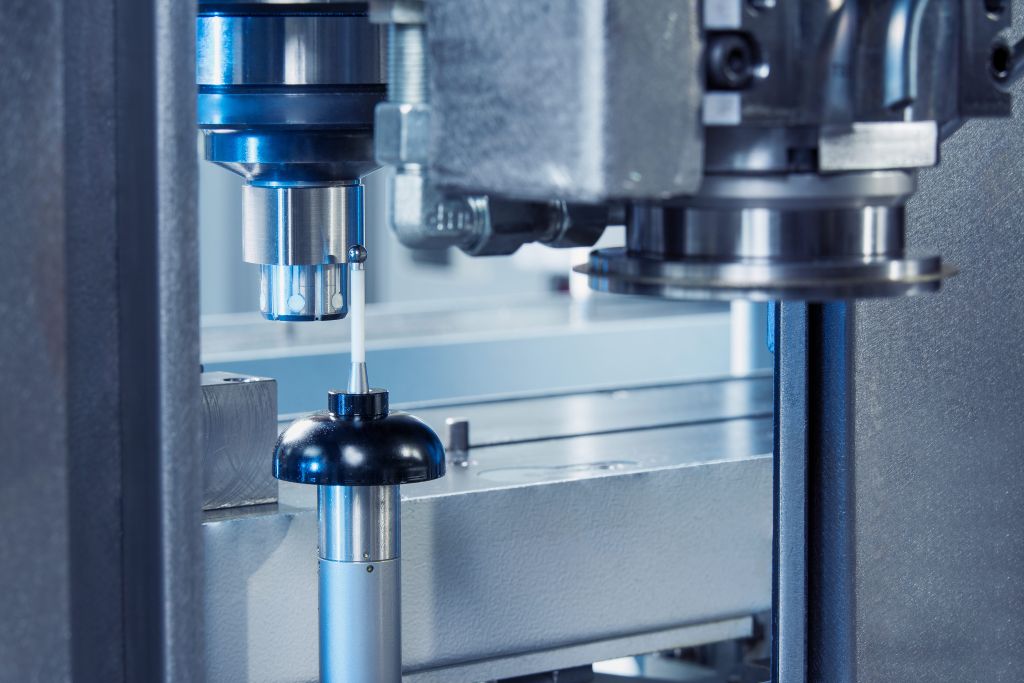
A body sound system enables the detection of contact between the grinding wheel and the workpiece as well as between the dressing roll and the grinding wheel. An adaptive process control monitors the grinding process in real-time and adjusts the feed rate to the current cutting conditions. Touch dressing is possible. The measuring probe positioned between the working area and the pick-up station is protected from contamination. Since the workpiece remains in the setup, measurements before, after, and between individual machining steps are possible.
Practical example: Sprocket in 35 seconds
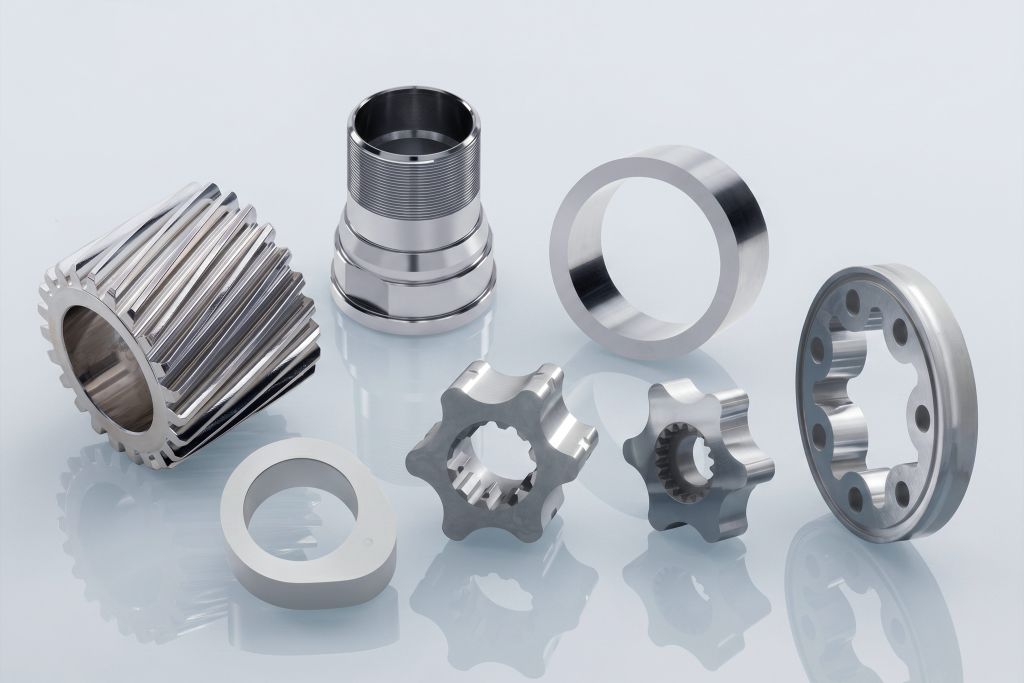
A specific application case demonstrates the capabilities: After automatic loading, the bore is finished ground with a CBN grinding wheel. Subsequently, two block steel holders process the flat surfaces through hard turning. Finally, the integrated measuring probe checks the quality. The entire process takes less than 35 seconds, of which about 10 seconds are for the workpiece change, 15 seconds for hard turning, and 10 seconds for grinding.
Technical specifications
Workpiece diameter up to 100 mm, chuck diameter up to 160 mm, swing diameter 210 mm. Travel paths: X = 895 mm, Z = 375 mm. Main spindle: 16.7 kW / 74 Nm (40% duty cycle), maximum speed 3,000 min⁻¹, spindle bearing Ø 80 mm.
The VL GT series
The VL 100 GT, the VL 200 GT (up to 200 mm), and the VL 350 GT (up to 350 mm) together form a continuous machine family with identical operating philosophy and compatible control software. Thanks to the modular design on the VL platform, identical base machines can be configured for different manufacturing tasks without the need for separate spare parts inventories or new operating concepts.
Contact: