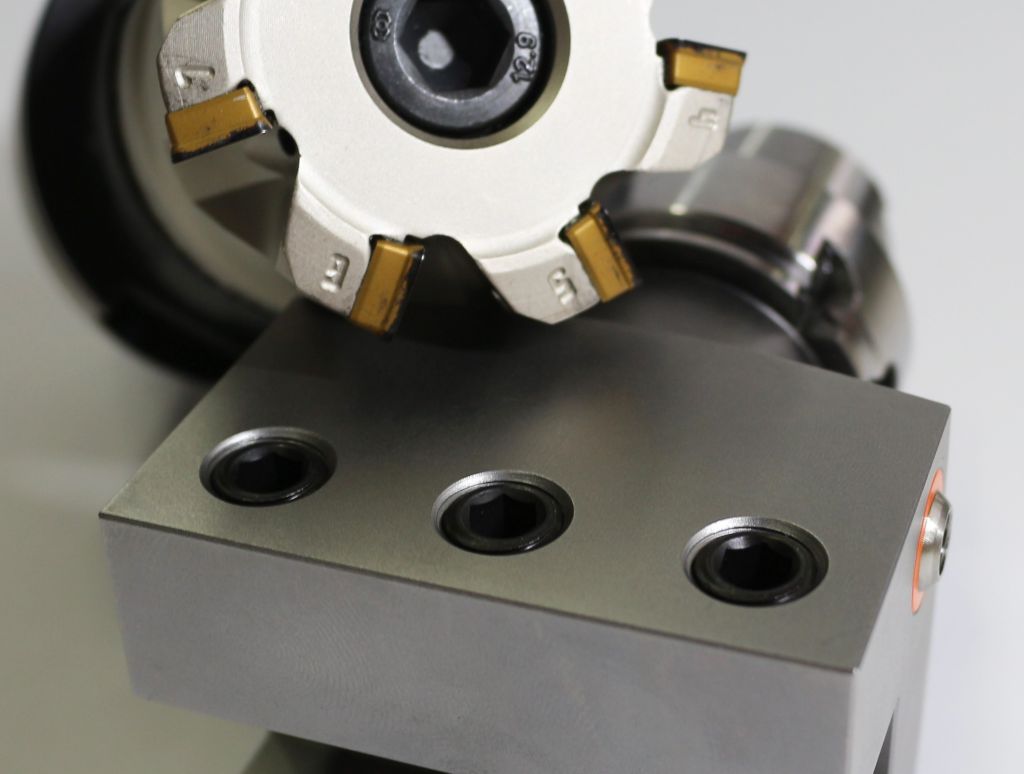
In the roughing of HSK holders made from alloy steel, Löcher GmbH achieved a small sensation: The machinists were able to reliably reduce the processing time for this work step by 90 percent. Thanks to ISCAR's MILL4FEED high-feed milling cutter and a new strategy, only two minutes instead of nearly 20 are needed per workpiece.
CNC turned and milled parts for machine builders, automotive suppliers, and customers from the metalworking sector in Germany are the specialty of Löcher GmbH from Westhausen in Baden-Württemberg. In addition to turning and milling, glass bead blasting, laser marking, and assembly are also part of the service spectrum of the contract manufacturer founded in 1974 in the basement of senior boss Anton Löcher. Werner Löcher runs the family business in the second generation, and with Luis Löcher, a machinist and aspiring mechanical engineer, the next generation is already on board. Löcher GmbH employs 25 staff and generates around three million euros annually.
"Highest precision, flexibility in custom manufacturing, and reliable and timely delivery of individual and series parts," summarizes Werner Löcher the expectations of the customers. This is accompanied by increasing demands on quality management, documentation, and traceability. "To meet these individual needs, we must offer short response times and also be able to manufacture economically in small batch sizes," explains the managing director.
That's why he became alert when Florian Schöffler, consulting and sales, application technician Martin Staudacher, and Uli Köhler, regional sales manager, presented ISCAR's MILL4FEED high-feed milling cutter and its application possibilities.
Immediately had the right project in mind
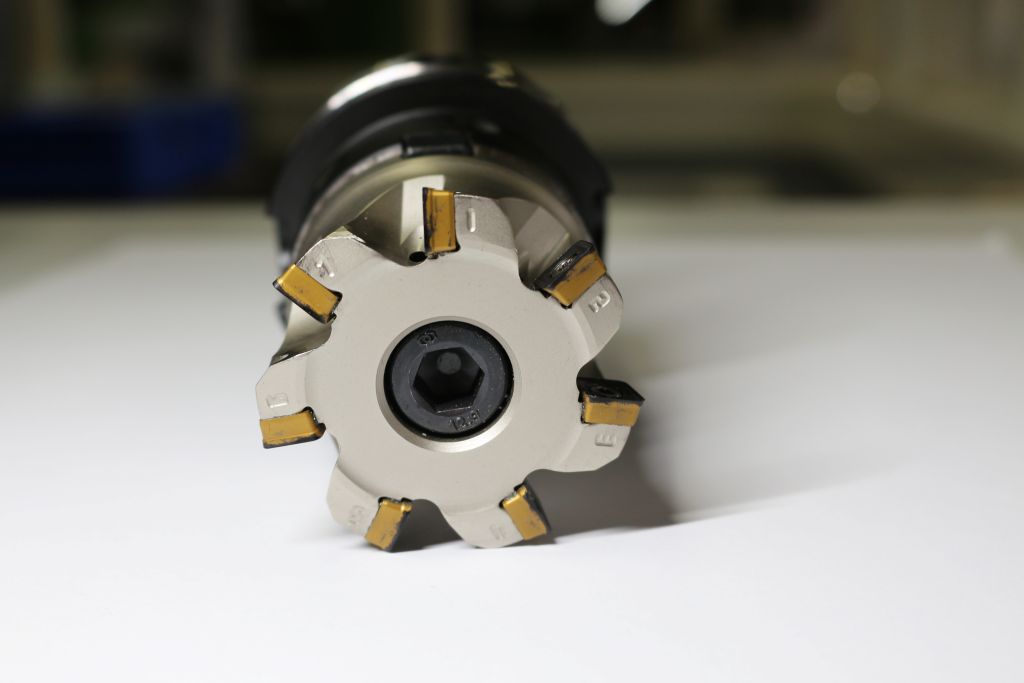
"With its different shanks, milling heads, and plate sizes, this high-feed milling cutter is very flexible," says Uli Köhler. "It opens up numerous new and economical machining possibilities for users in all materials." The MILL4FEED is equipped with single-sided indexable cutting inserts (WSP) with four cutting edges. Due to its positive rake angle, the tool cuts very smoothly. The force impact on the cutter occurs predominantly in the axial direction.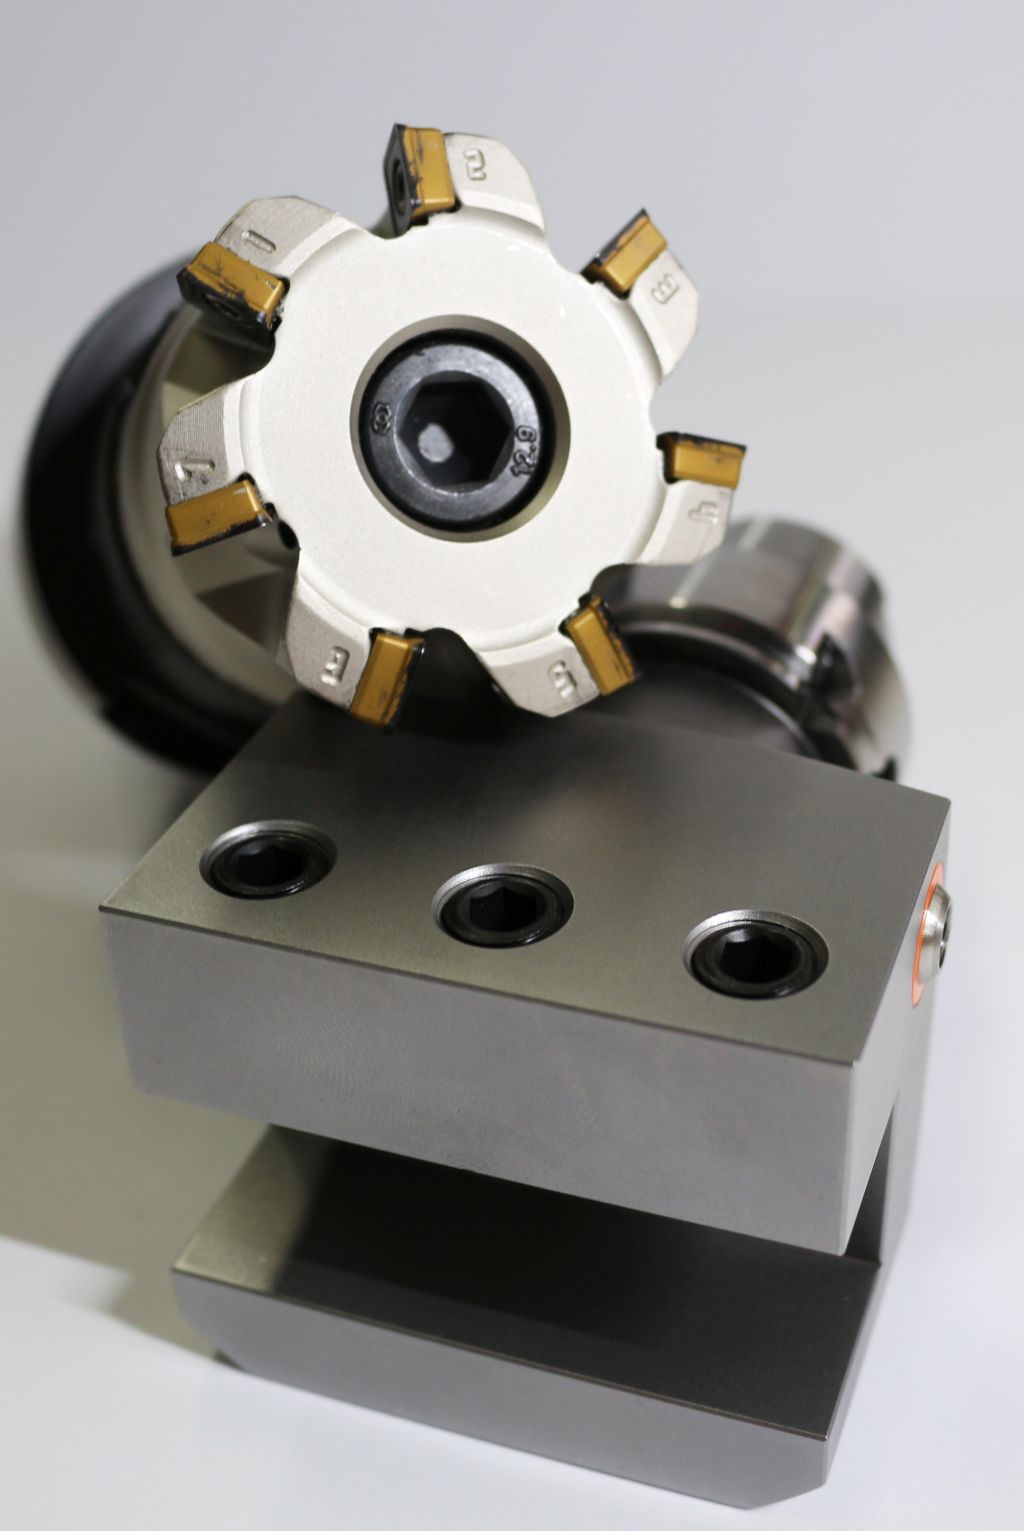
This enables low-vibration processes even with unstable clamping. The WSP are available in five different geometries and cutting material types. Users achieve a depth of cut of up to three millimeters and a maximum feed of two millimeters per tooth. The cutting edges are particularly stable and offer long tool life even with interrupted cuts.
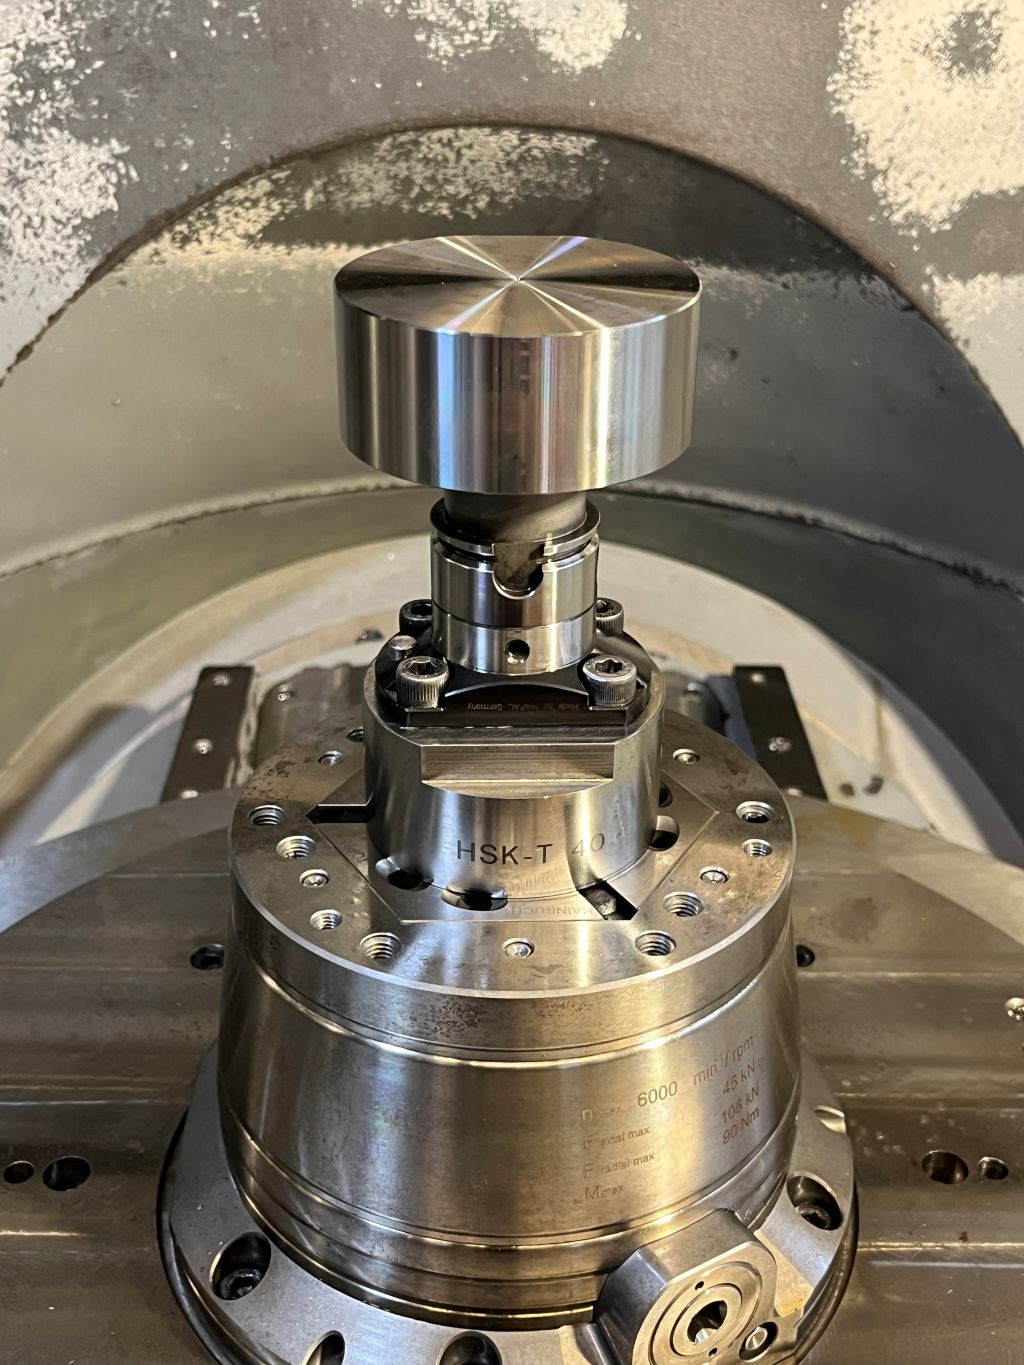
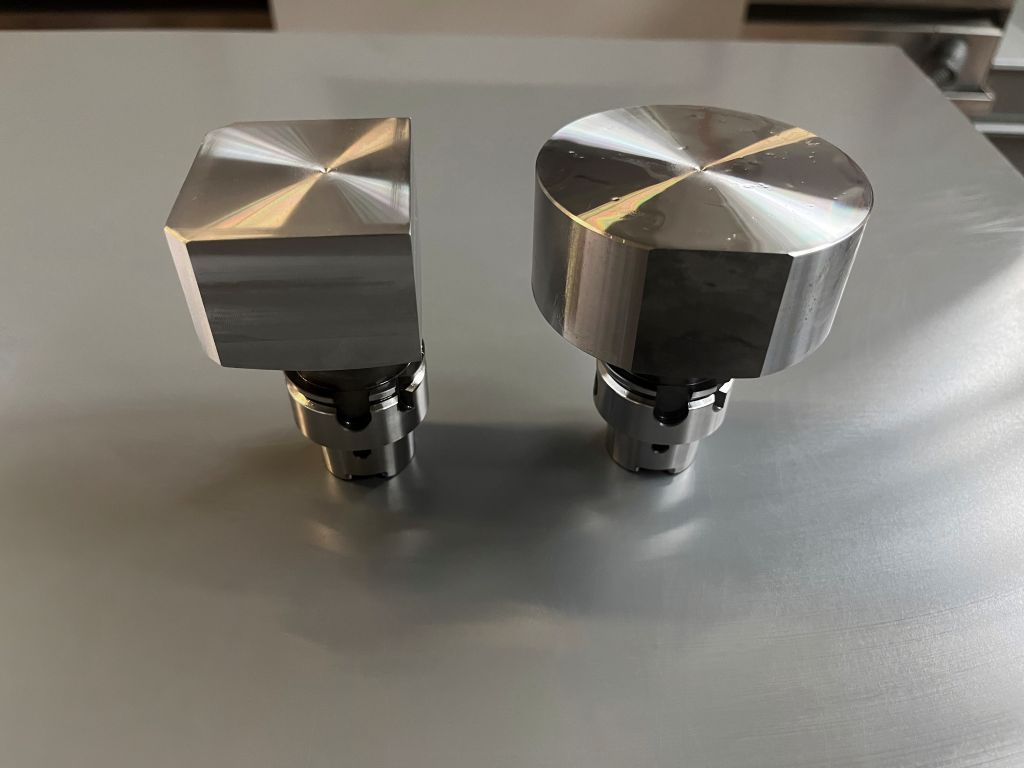
"I was initially skeptical due to the high cutting pressure, but after the first test runs, I immediately had the right task in mind," says Werner Löcher. "The roughing of a small series of HSK40 turning holders made from 42CrMo4, tempered to 1,200 megapascals. In previous batches, we practically ground away our profit due to the long processing time."
New strategy reduces processing time
Löcher manufactures the parts from A to Z themselves. The basis is three-meter bar material with a diameter of 80 millimeters. After turning and shaping the HSK holder, the four side faces are milled into the round blanks, and they receive their final shape. Until now, Löcher used a solid carbide milling cutter from an ISCAR competitor for this. This cutter trimmed the four sides to be machined with a feed of 0.2 millimeters per tooth.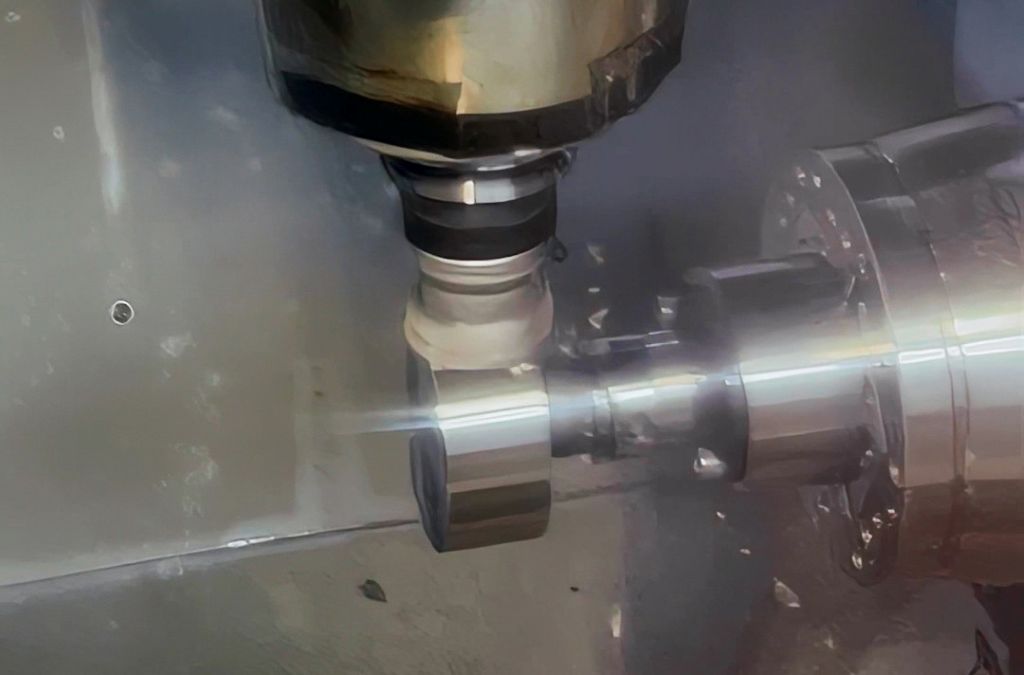
More was not possible due to occurring vibrations. "That took forever, and then there were 20 minutes on the clock per holder," recalls Werner Löcher. However, the safety-oriented programming, which included many empty movements, weighed heavier than the low tooth feed.
"We looked at the process and proposed a new processing strategy," says Martin Staudacher. "Instead of contouring and moving around a lot, we recommended pendulum face milling in the same and opposite direction."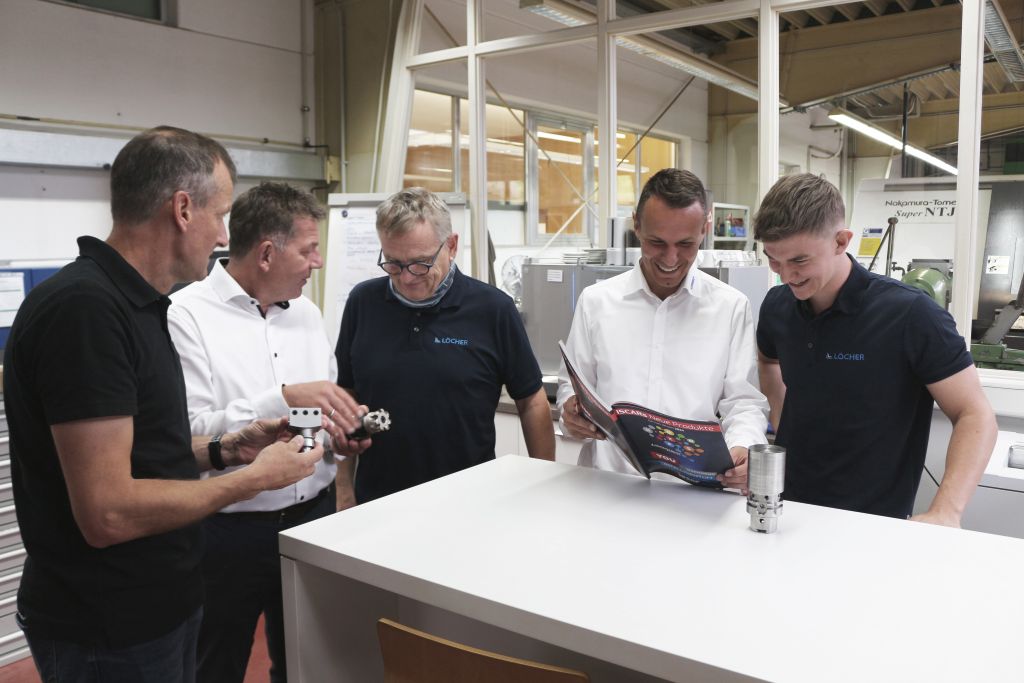
For corresponding efficiency, the MILL4FEED with a diameter of 52 millimeters should be used. It has seven effective teeth and a cutting width of 36 millimeters. Its 09 WSP from the TiAlN coated fine grain type IC808 with HP chip former ensure a vibration-free, smooth cut with low cutting pressure, high wear resistance, and top surface quality. With the new solution, Löcher was able to increase the feed per tooth to 0.94 millimeters.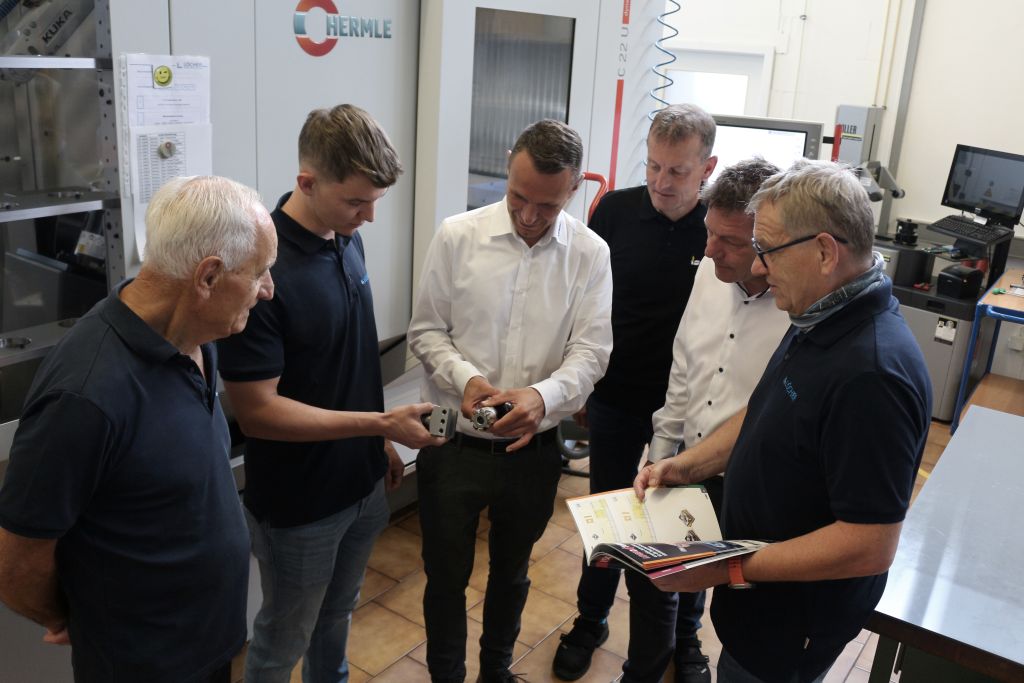
"Due to the high speed, we were initially a bit worried that the part with the small HSK would fly out of the clamping," says Florian Schöffler. This concern was unfounded – the desired result was achieved: more efficiency. The new solution reduces the processing time per component by 90 percent.
Faster, more flexible, safer
The Löcher team could hardly believe at first that the roughing now only takes two minutes.
"We repeated the run twice to be sure," laughs Werner Löcher. "I've never experienced such a reduction at once. It's like a lottery win."
Especially the new processing strategy makes the difference: Many approach and return movements are eliminated, and the tool remains almost permanently in engagement. "The machine is practically always cutting. No idle times, no unnecessary movements," praises Luis Löcher. "And this with a process reliability that really surprised us."
In addition, the MILL4FEED opens up additional possibilities for Löcher GmbH in machining.
"The cutter is simply top for the right application," summarizes Werner Löcher. "We will definitely use it more often in the future because it brings us flexibility and safety."
The partnership between Löcher and ISCAR has existed for more than 30 years and it works better today than ever. Werner Löcher praises: "At ISCAR, we have direct contacts who know what they are doing. It's not just about the price, but about performance, and the consulting is on a completely different level."
Contact: