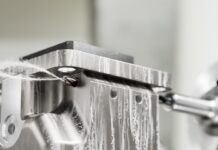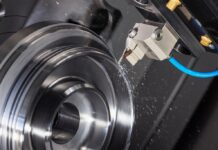
Components with small, precise internal fits are among the particularly challenging tasks in development and manufacturing, for example in tool and fixture construction, valve and fluid technology, or in precision components of machine and drive engineering. Conventional hard turning as an established finishing process can reach its limits, especially with small inner diameters, depending on the material, geometry, tolerance, and quality requirements. The smaller the hole, the smaller and more delicate the internal tool must be. Tool wear, resulting tool life, and the fundamental process stability also prove to be relevant economic factors, as they directly affect the piece costs. In these cases, finish grinding proves to be a tried-and-true and reliable alternative. However, conventional processes also show noticeable limitations here, both qualitatively and economically.
Grinding Finish: When One More Step is One Step Too Many
Traditionally, the grinding process takes place on a separate grinding machine. This means in practice: The desired component is machined on the lathe, then removed, clamped on the grinding machine, and, after the internal fit has been ground, further processed as needed. The machine change not only represents an additional manual step and thus a question of cost-effectiveness, but also reveals fundamental quality risks: The re-clamping increases the risk of positional and runout errors, which are particularly relevant for small fits.
GrindLine: A Proven Method Reimagined
With the new GrindLine, the expert in the development, manufacturing, and distribution of high-precision tool holders for lathes and milling machines, tool holder systems, and accessories EWS offers an alternative to both the limited suitability of hard turning and the conventional use of grinding on a separate grinding machine.
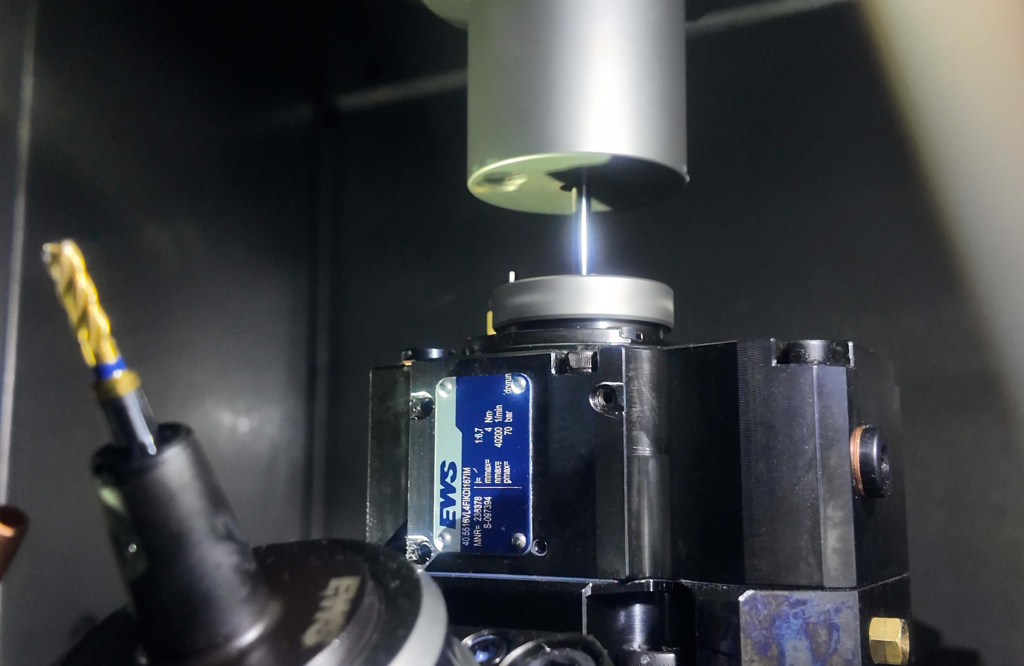
GrindLine is a driven tool holder with high-speed spindle for finish grinding directly on the lathe or turning-milling center.
This eliminates not only the critical re-clamping and the associated risks, as the position of the ground internal fit remains related to the already machined geometry, but the entire manufacturing process is optimized in favor of manufacturing quality and cost-effectiveness.
The actual technical peculiarity, however, is the drive of the GrindLine, which occurs purely mechanically. This is not simply an electrically operated grinding unit with a cable or an external power supply. The high-speed spindle is driven mechanically via the AGW interface of the tool turret. Thus, not only is the re-clamping to a separate grinding device eliminated, but no machine conversion is required either. Moreover, GrindLine is more compact than generator-driven units and is suitable for a wide range of different machines. Nevertheless, the high-speed spindle with ceramic hybrid bearing achieves up to 40,200 min⁻¹ through the integrated gearbox and enables the required cutting speeds with small grinding tools.
A Solution for the Workshop, from the Workshop
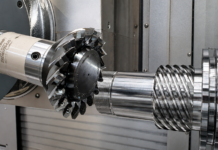
With EWS.GrindLine, EWS expands the EWS.Special Solutions product line with a new tool solution for finish grinding of small inner diameters. EWS.Special Solutions bundles application-related tool solutions for gear milling, keyway cutting, polygon machining, high-speed threading, and high-speed micro-machining as well as internal boring heads.
The development is not the result of sober product marketing, but arose as a practical solution for a specific machining case in EWS's own manufacturing. As described, the conventional tools and methods of hard turning proved to be technically and economically unsuitable for the tasks of finish machining small inner diameters. This provided the idea for the development of an alternative method, which was ultimately advanced to the market-ready solution GrindLine.
EWS.GrindLine made its debut at AMB 2026 in Stuttgart. The initial variant was presented as an axial BMT55 version. Further BMT and VDI versions as well as straight and angled designs are being examined on a project basis and implemented where technically feasible.
Contact: