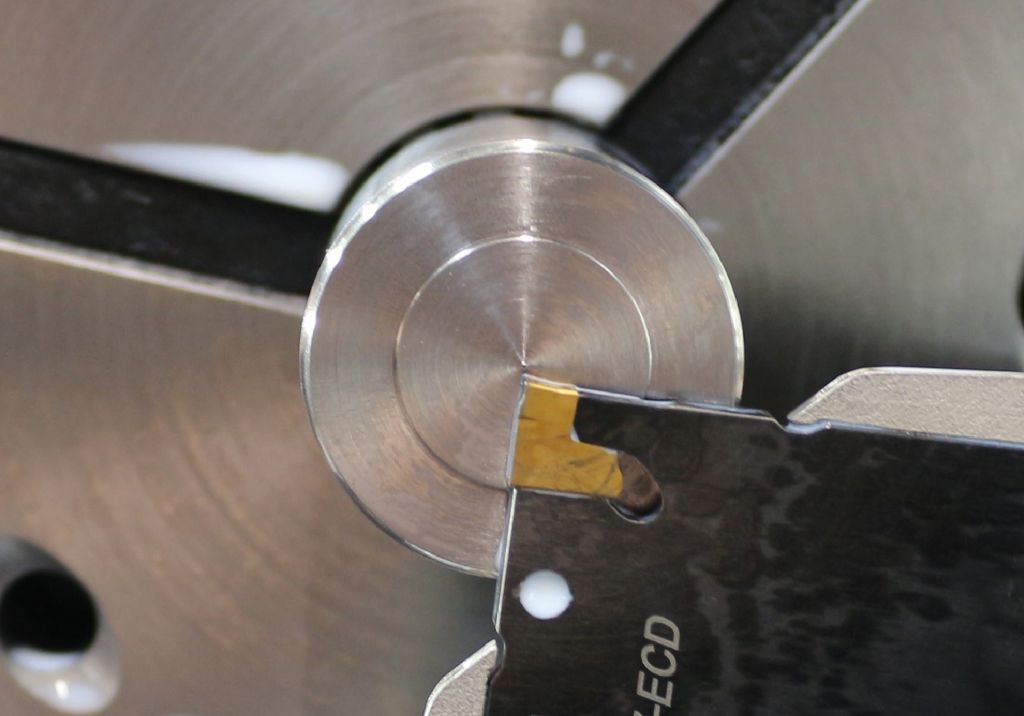
When it comes to turning, often a detail determines process reliability or scrap: the chip former. This makes it much more than just an additional feature of the cutting edge – it is an integral part of the tool. Which of the many different chip formers is the right one depends on the material, cutting parameters, process, and machine.
Chip formers are the geometric elements on the cutting surface of the insert that control exactly that: chip formation, chip flow, and chip breakage. Their task sounds simple, but it is quite demanding. The chip former must redirect and shape the chip so that it rolls up cleanly, breaks as short as possible, and is safely discharged from the engagement area without jamming, snagging, or bouncing back onto the workpiece surface. If this fails, scratches and grooves appear on the surface, and users struggle with increased wear, cutting edge damage, and machine downtimes.
"When a long chip wraps around the tool and brings the machine to a standstill, it is not only annoying but especially a real problem when turning," says Frederik Schmalbach, product manager for Non-Rotating Tools at ISCAR. "Chip removal is a determining factor for process reliability, tool life, and surface quality here."
Various reasons for use
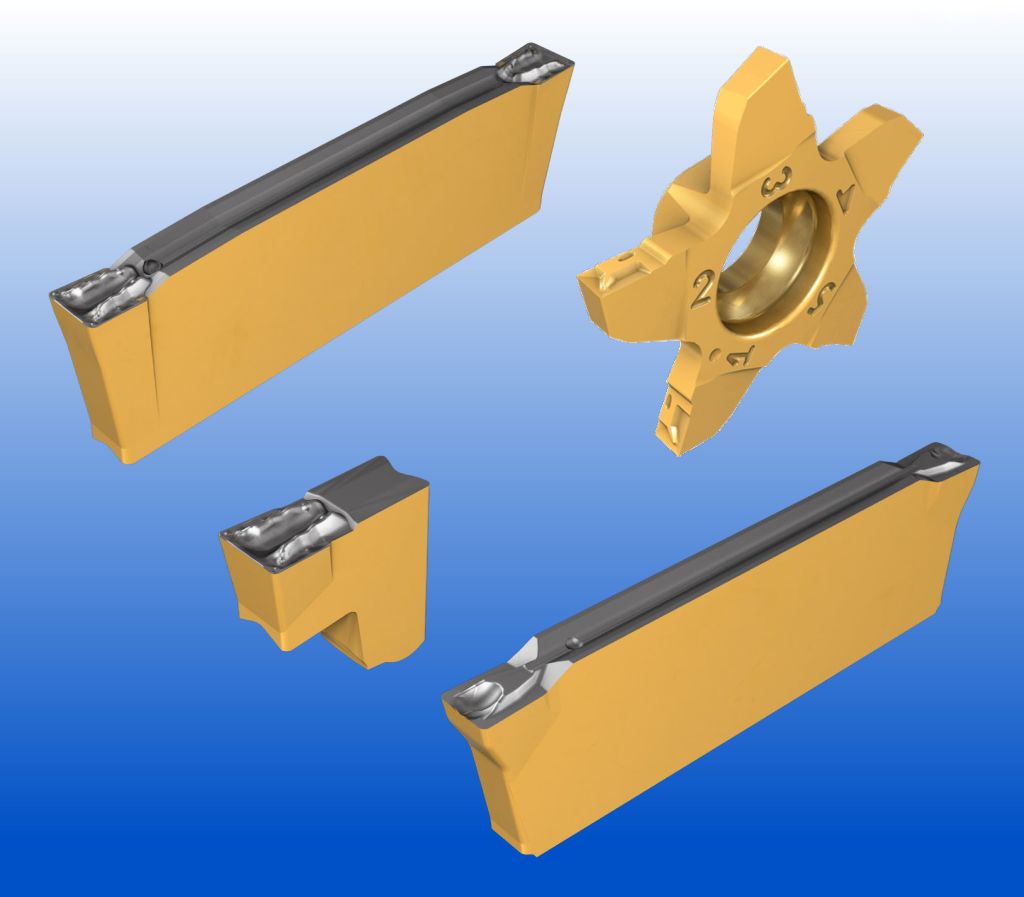
In turning, chip removal is usually straightforward. The chip has space and can easily flow out sideways. In contrast, when turning and parting, the tool radially plunges into the workpiece. "The deeper the engagement, the tighter the groove," explains the product manager. "The chip has hardly any space and must behave in a controlled manner from the very first moment."
Tough materials like low-alloy steels, stainless steels, and ductile alloys produce long, band-like chips that do not break without a chip former. The chip former tightly rolls the chip and breaks it early. The result: free chip removal, stable cutting conditions, and uniform wear.
"Chip formers are used whenever the material to be processed tends to produce long, tough chips, when narrow turning widths or deep grooves are being machined, when automated processes with high runtime are required, and when chip wrapping and chip accumulation have proven to be a problem," lists Frederik Schmalbach. "Also everywhere where surface quality and dimensional accuracy do not tolerate deviations, the appropriate chip former geometry is not an optional detail."
Factors for the perfect chip
Chip formers can be distinguished by their operating principle, geometry, and application area. Geometric chip formers are directly integrated into the chip surface of the cutting insert. Typical forms include chip grooves, chip guiding steps, nose shapes, and profiled chip pockets. They mechanically influence how the chip deforms, rolls, and breaks.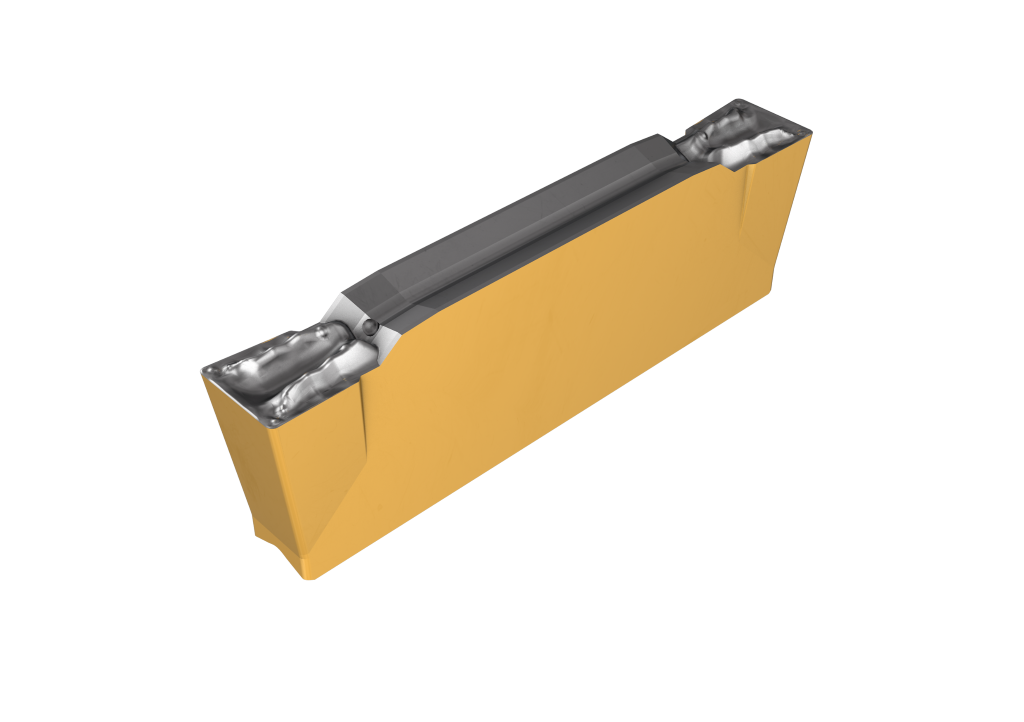
Material-specific chip formers are tailored to typical material properties. A chip former for ISO-P steels is designed differently than one for ISO-M stainless steels or ISO-S high-temperature alloys. Chip formation, cutting forces, and friction behavior vary significantly depending on the material group.
Process-specific chip formers take into account the respective machining case. External turning, internal turning, parting, and groove turning place different demands on the chip former.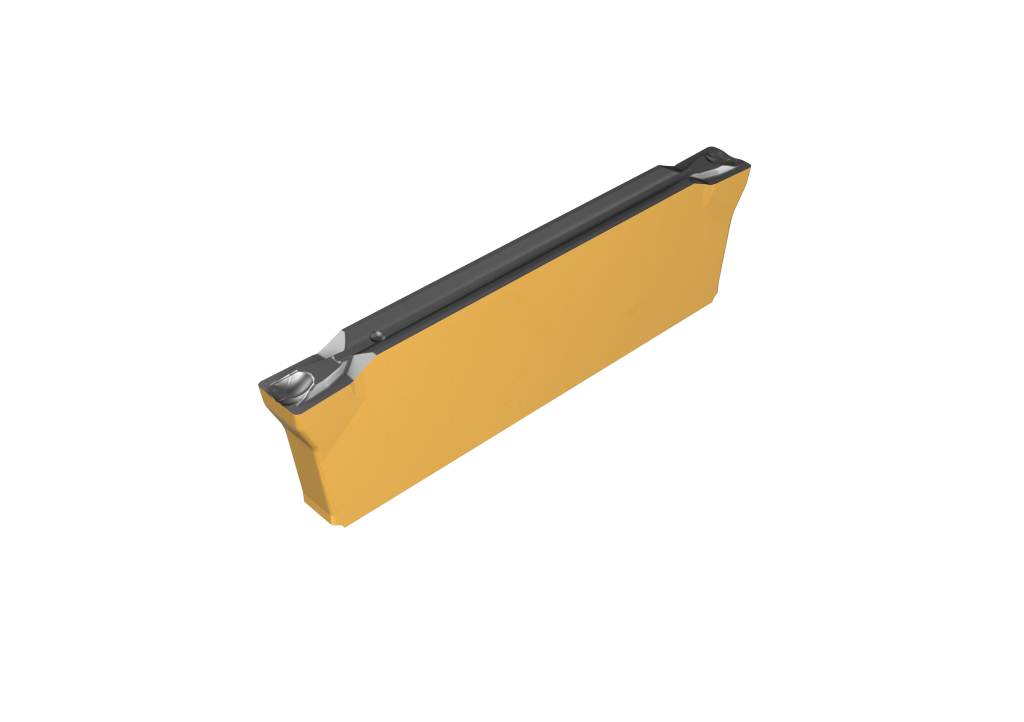
"In practice, however, these three categories are rarely sharply separated," says Frederik Schmalbach. "Modern chip formers combine all three aspects in a geometry that is specifically tailored to a tool system, a workpiece group, and a machining case."
To provide the user with the appropriate chip former for every turning task, ISCAR has consistently expanded its portfolio in recent years.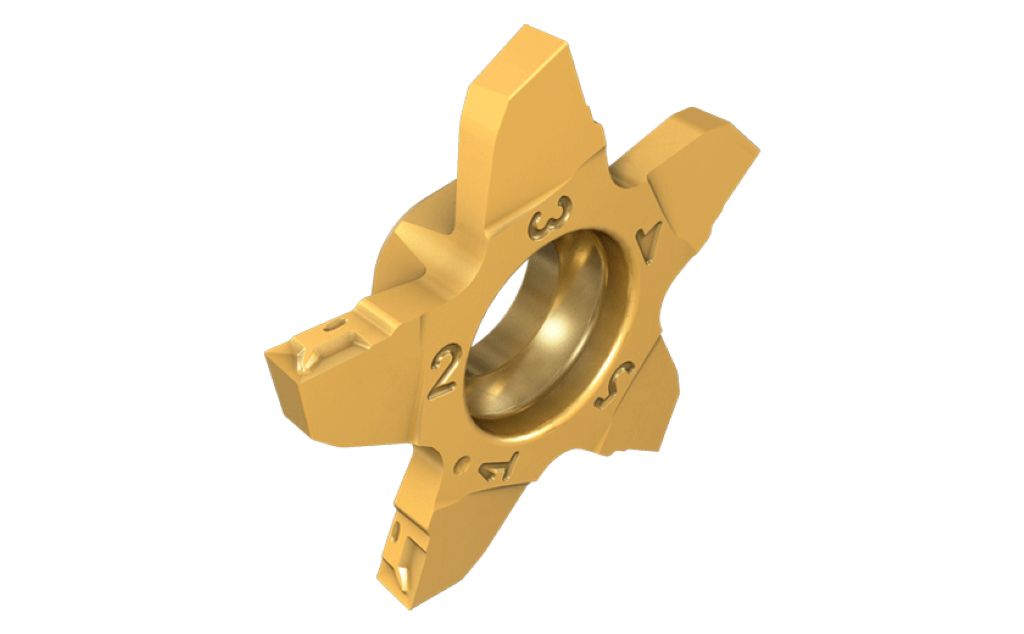
"Some of these are actual new developments that have found their way from the special area into the standard, while others are existing geometries that we were able to transfer from other fields to turning," says Frederik Schmalbach.
In the search for chip formers, ISCAR supports users not only with personal advice but also with its "Chip Former Guide," which can be requested from the relevant advisor.
The T-chip former: first choice for chip control
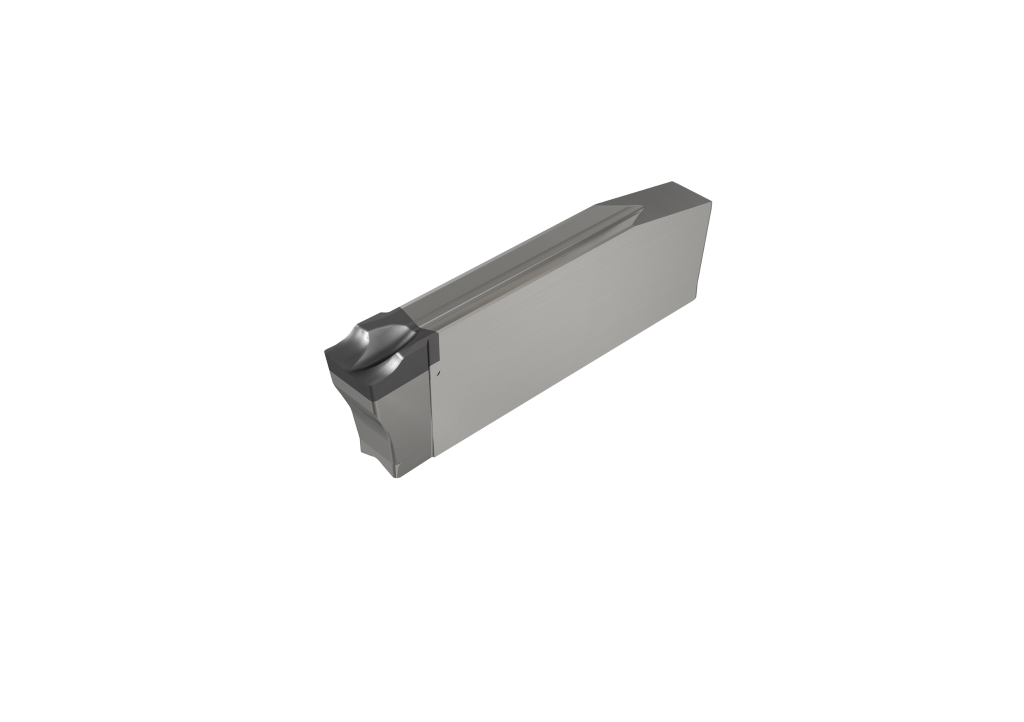
The T-chip former has its roots in turning and has proven itself on the cutting edges of the CUT-GRIP series. "It goes through metal as if it were cotton," says Frederik Schmalbach enthusiastically. "We simply had to adapt it for our DO-GRIP and TANG-GRIP cutting inserts." The T-chip former features a positive chip pocket, a stable cutting edge, and a chip deflector. This is positioned close to the cutting edge and the corner radius, allowing for top chip control. The chip is rolled up in a controlled manner and reliably breaks short.
The stable cutting edge of the T-chip former also allows for partial widening of grooves, meaning lateral turning after the first plunge. This geometry thus covers two typical machining cases.
B-chip former: for tough materials and built-up edge formation
The new B-chip former offers the appropriate geometry for machining particularly tough materials with DO-GRIP, TANG-GRIP, and PENTACUT cutting inserts. Its high chip deflector guides the chip over a longer distance and rolls it in intensely. The sharp cutting edge transitions into a soft-cutting chip pocket and prevents vibrations. To prevent the chip from getting tangled in very tough materials, the B-chip former also cuts it very well laterally. "The B-chip former is our answer to materials that cause problems for classic geometries, such as 100Cr6 or similarly tough bearing steels. Without a suitable chip former, built-up edges and uncontrolled chip removal quickly occur," says Frederik Schmalbach.
NX-chip former for PENTA 17: For short chips
The PENTA 17 is the ISCAR system for small components. Until now, the five-edged insert was only equipped with fillets. These produced very long chips that could wrap around the tool and workpiece. To tackle this challenge, ISCAR developed the NX-chip former. Its geometry features a sharp cutting edge that transitions into a soft-cutting chip pocket. "With the new NX-chip former, the chips break short, and we give the user precise chip control in small part machining," says the product manager.
J-chip former on PKD: High performance with non-ferrous metals
The latest innovation in the ISCAR chip former program for grooving is also the most technically demanding: PCD cutting inserts with the J-Chip Former for the DO-GRIP system for machining non-ferrous metals. 'PCD and the J-Chip Former are a logical combination. PCD provides sharpness and wear resistance, while the J-Chip Former ensures that the chip flows controlled despite high cutting speeds,' says Frederik Schmalbach.
The laser-embedded J-Chip Former models the chip precisely and reproducibly well. Aluminum and copper alloys, brass, non-metals, and composite materials can be processed with it.
'Choosing the right chip former for a task does not follow chance, but clear technical criteria,' summarizes Frederik Schmalbach. 'Those who understand this gain a real lever for more process reliability, longer tool life, and better surface qualities.'
Contact: